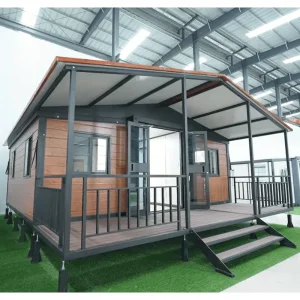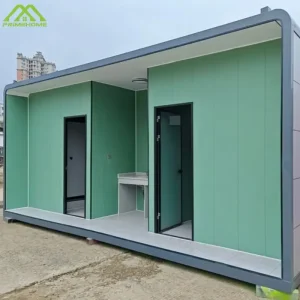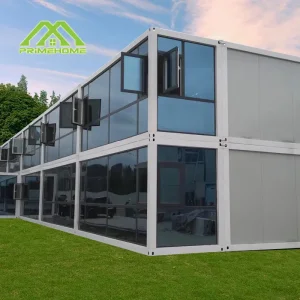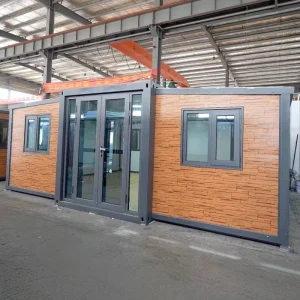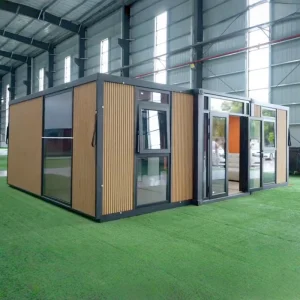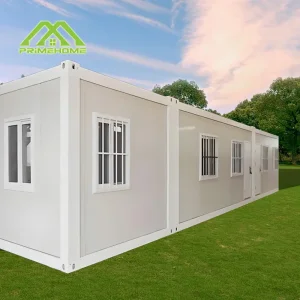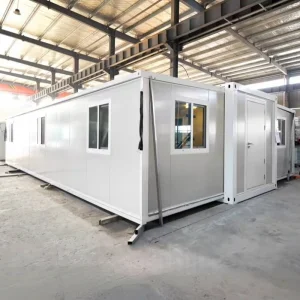
Featured Modular & Double-Storey Enclosures
Explore high-performance modular units engineered for structural duplex stacking, rapid site deployment, and architectural durability.
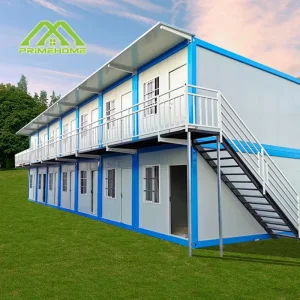
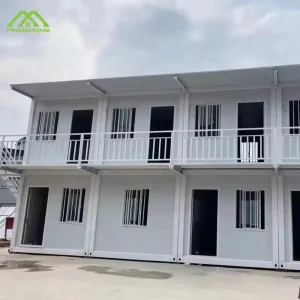
Global Commercial & Industrial Status of 2-Storey Modular Structures
Vertical spatial optimization has transitioned multi-storey prefabricated volumetric structures from temporary shelters into permanent, code-compliant institutional assets.
Land Density Optimization
In high-density industrial and urban fringe zones, land footprint restrictions drive demand for multi-tier volumetric buildings. Standard 2-storey modular stacking provides an exact 100% floor area expansion over identical ground plots without requiring intensive, permanent foundation engineering.
High-Yield Hospitality Deployments
Modern luxury eco-resorts, glamping destinations, and remote retreat providers utilize multi-level designs to isolate social spaces downstairs while preserving elevated, panoramic bedroom suites upstairs. Prefabricated modules ensure quick setup and rapid capital return.
Rapid Infrastructure Operations
Large infrastructure developers leverage stackable two-storey units for temporary managerial field offices, staff quarters, and high-spec clinics. These structures meet international fire safety and wind-load criteria while retaining the versatility to be dismantled and reused on future sites.
Engineering Evolution & Structural Trajectories
Transforming steel boxes into refined living architecture requires systematic innovation across load distribution, envelope performance, and circular production methods.
Structural Physics: Vertical Load Transfers
Two-storey modular engineering relies on specialized corner-casting columns and reinforced cold-formed tubular steel skeletons. By channeling seismic lateral drift and high dead loads through ISO twist-lock corner interfaces, the structural frame maintains stability even under wind speeds up to 120 km/h (Beaufort scale 12).
Envelope & Thermal Barrier Engineering
Eliminating thermal bridging across steel members is critical for multi-level buildings. Modern production lines utilize continuous high-density PIR/PUR injection panels, exterior rockwool ventilation cavities, and Low-E argon-filled tempered double glazing. This keeps internal heating and cooling requirements aligned with strict building standards like EU EN 1090 and Title 24.
Factory Integration & MEP Systems
True modular efficiency demands factory-installed mechanical, electrical, and plumbing (MEP) systems. Vertical conduits, waste drainage stacks, and plug-and-play high-voltage connections are pre-aligned using laser-guided jigs during fabrication, cutting final field installation time by over 70%.
Tailored Regional Application Scenarios
How two-storey modular buildings meet specific climatic, regulatory, and practical needs across diverse global markets.
Arid & High-Solar Zones (Middle East & Australia)
Equipped with reflective exterior finishes, ventilated sub-roof canopies, and double-glazed solar control windows. Dual-floor accommodations feature integrated, low-draw VRF cooling lines capable of operating reliably in ambient heat exceeding 50°C.
Sub-Zero & High-Snow Climates (Nordics & North America)
Reinforced roof trusses handle static snow loads up to 2.5 kN/m². Wall cavities are packed with 150mm stone wool, paired with thermal decoupling breaks and interior floor heating systems to keep interior environments comfortable and cost-effective to heat.
High-Humidity & Island Environments (Southeast Asia & Caribbean)
Components receive complete hot-dip zinc galvanization (minimum 275g/m² coverage) alongside C4/C5 marine-grade fluorocarbon anti-corrosion coatings. Waterproof vinyl finishes, sealed flashings, and mold-resistant wallboards protect long-term structural integrity.
Technology Roadmap: The Future of Modular Architecture
A structured timeline detailing our engineering milestones and sustainability initiatives from 2025 to 2030.
Standardizing six-axis robotic framing cells to guarantee millimeter-tight corner tolerances and seamless interlocking alignment on multi-level units.
Factory-mounting high-efficiency BIPV (Building Integrated Photovoltaics), integrated lithium storage racks, and graywater recycling cassettes for true self-sufficiency.
Transitioning to 100% recyclable lightweight green steel alloys, zero-VOC bio-insulation cores, and verified carbon-neutral factory operations.
Embedding internal structural sensor arrays to monitor real-time wind shear, foundation settling, humidity shifts, and preventative maintenance metrics.
Macro Turnkey Solutions for Developers & Procurement Leaders
A proven, end-to-end manufacturing and logistics process designed for corporate clients, resort operators, and large contractors.
1. Architectural Engineering & Code Alignment
Our in-house design team converts preliminary architectural sketches into full CAD/BIM blueprints, calculating dead/live loads, thermal values, and electrical configurations to match destination-specific building codes.
2. Mass Precision Fabrication (Suzhou Base)
With 28,000 m² of factory space and capacity exceeding 5,000 units monthly, we fabricate steel frames, install pre-plumbed wet pods, and apply finishes under rigid quality-control protocols.
3. Compact Export Logistics & On-Site Stacking
Units are packed as flat-pack packages or protected volumetric units to maximize 40HQ ocean container capacity. On site, crane rigging guides, step-by-step schematics, and factory field supervisors ensure safe, smooth assembly.
Frequently Asked Technical & Sourcing Questions
Direct technical guidance covering structural integrity, import logistics, and long-term performance.
How is structural wind and seismic safety ensured on two-storey stacked container setups?
Two-storey modular systems utilize high-tensile cold-formed steel frames with reinforced corner columns. Structural connection between floors is secured via standard ISO container lock blocks and heavy-gauge structural connector plates bolted directly to the corner castings. This engineering easily accommodates wind loads up to 120 km/h and handles Seismic Zone 7 to 8 dynamics, confirmed through FEA stress-strain testing prior to manufacturing.
What foundation preparation is required for double-storey modular installations?
Because structural loads are channeled downward through the four main vertical corner columns, a full concrete slab is rarely necessary. Point footings (concrete piers) aligned beneath each corner block are often sufficient for stable soils. For softer or uneven ground, strip footings or adjustable screw-pile helical foundations offer a reliable, fast, and eco-friendly foundation alternative.
How is inter-floor acoustic transmission (impact and airborne noise) mitigated?
To prevent footstep impact and airborne sound transmission between upper and lower levels, our two-storey designs incorporate a multilayered floating floor assembly. This setup pairs an integrated high-density MGO or cement-fiber subfloor with an acoustic elastomer isolation mat, dense rockwool acoustic insulation, and an air-gap acoustic ceiling hung on the lower unit, consistently achieving Sound Transmission Class (STC) ratings above 52 dB.
Can customized layouts, balconies, and internal/external staircases be incorporated?
Yes. We offer fully customizable architectural floor plans. Factory options include external structural steel stairways, cantilevered balconies with safety glass railings, internal spiral stairs, open-concept living rooms, and integrated terrace systems. All penetrations and connection brackets are pre-welded and reinforced directly in the factory to preserve envelope waterproofing.
What is the realistic service lifespan of a two-storey container building?
Built with hot-dip galvanized steel frames and premium anti-corrosion protective coatings, our modular structures feature a design life of 25 to 50+ years depending on site conditions and chosen envelope materials. Periodic maintenance matches conventional light-steel residential structures, providing a reliable, low-maintenance building solution.
Advanced Expandable, Glamping & Modular Accommodations
Complete your development plan with our expandable suites, luxury cabins, and multi-bedroom living modules.