Custom Residential Container Homes Manufacturers & Supplier
Pioneering high-durability modular living environments, expandable structures, and architectural eco-cabins engineered to international residential building codes for institutional developers, hospitality conglomerates, and municipal entities.
High-Performance Residential Product Lineup
Pre-engineered structural modules manufactured in our ISO-certified Suzhou facility, featuring plug-and-play mechanical infrastructure, custom internal layouts, and turn-key site integration.
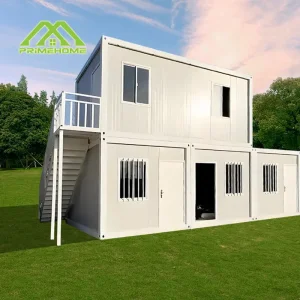
Custom 20-year warranty mobile prefabricated houses complete with kitchen and bathroom
Configure Unit Specs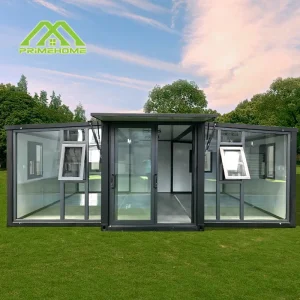
20FT Galvanized steel double-wing expandable container home for camps and residential use
Configure Unit Specs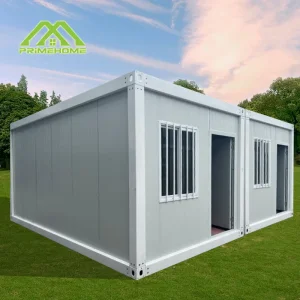
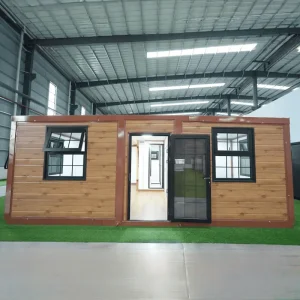
20ft portable prefabricated flat pack house with high-density steel structural chassis
Configure Unit Specs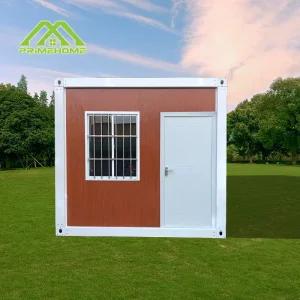
Affordable 40-foot expandable modular container residence with high thermal envelopes
Configure Unit Specs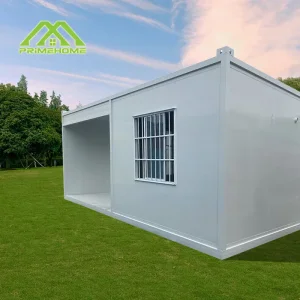
Modular 20ft/40ft expandable container living pods with customizable interior layouts
Configure Unit Specs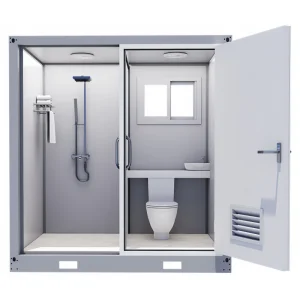
Factory pre-finished modular luxury restroom pod with glass-enclosed shower suite
Configure Unit Specs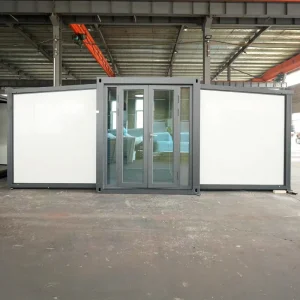
Wholesale 20FT modular expandable dwelling configured for minimalist single-unit apartments
Configure Unit SpecsEvolving the Global Paradigm of Residential Construction
Addressing structural labor deficits, climate-resilient building envelopes, and circular manufacturing standards with automated factory-built architecture.
Structural Integrity & Steel Alloys
Unlike repurposed shipping boxes prone to chemical contaminants and structural fatigue, PrimeHome utilizes Q235B and high-tensile galvanized cold-formed steel frames engineered to resist seismic zone 8 accelerations and wind pressures up to 180 km/h, verified via finite element analysis.
Thermal Envelope Science
Thermal bridging elimination is central to our residential envelopes. We incorporate continuous polyisocyanurate (PIR) cores, rockwool insulation (class A1 non-combustible), and Low-E argon-filled argon double glazing to guarantee low U-values compliant with European EnEV and California Title 24 standards.
Turn-Key MEP Factory Pre-Rigging
Every living pod leaves our floor with factory-integrated mechanical, electrical, and plumbing (MEP) systems tested under real loads. Conduit routing, circuit breakers, PEX water lines, and integrated graywater manifolds are pre-certified for instantaneous plug-and-play field hookups.
Macro-Industry Solutions for Enterprise Developers
Mitigating the challenges of commercial development cycles through scalable off-site modular manufacturing.
Boutique Hospitality & Eco-Resorts
Rapid deployment of luxury Apple Cabins and futuristic Space Capsules that achieve complete site activation within 30 days, bypassing complex on-site foundation footprints and environmental disruption in remote scenic areas.
Municipal ADU & Urban Infill
Addressing national housing crunches through turnkey Accessory Dwelling Units (ADUs). Compact dimensions allow standard flatbed transport, crane drop-in positioning, and immediate municipal utility interconnects.
Disaster Recovery & Civil Defense
Ultra-fast folding and expandable shelters manufactured in high volumes. Up to 6 units ship in a single 40ft HQ container, erecting in under 15 minutes per module to supply secure, hygienic living centers in catastrophe zones.
Remote Mining & Infrastructure Camps
Modular workforce villages combining private insulated residences, multi-stall sanitation blocks, commercial galleys, and admin pods designed for harsh arctic cold or hyper-arid desert deployment.
Localization Support, Permitting & Code Adherence
Cross-border modular housing success hinges entirely on granular compliance with municipal building codes and national electrical/sanitary standards.
North American Standards (IBC / IRC)
PrimeHome configures structural steel members, snow load roof deflection calculations, and UL-listed electrical hardware to satisfy the International Residential Code (IRC) and HUD requirements. Structural calculation sheets signed by licensed professional engineers (PE) can be coordinated for municipal plan check approvals.
European Union Directives (CE & EnEV)
Factory-applied CE marks for all structural load-bearing components (EN 1090-1), structural thermal performance validation, low-VOC formaldehyde-free indoor wall cladding materials, and EN 60335 compliant electrical distribution systems for seamless European commercialization.
Australasia (BCA & WaterMark)
Full customization to Australian and New Zealand building standards (AS/NZS 1170 wind/cyclone regions, AS 3000 electrical wiring regulations), along with WaterMark-certified sanitary fixtures and termite-resistant composite floor sub-bases for Oceanic markets.
Modular Engineering Roadmap: 2026–2030
Leading the next industrial leap in digitalized fabrication, self-sustaining microgrids, and intelligent living envelopes.
BIM-Driven DfMA Fabrication
100% cloud-synced Building Information Modeling (BIM) integrating Design for Manufacture and Assembly (DfMA), reducing fabrication tolerances to under 1.5mm across all chassis weld points.
Net-Zero Energy Envelopes
Integration of ultra-thin vacuum insulation panels (VIP), aerogel window glazing, and pre-wired rooftop BIPV (Building-Integrated Photovoltaics) with residential battery energy storage (BESS).
Smart IoT Biospheres
Embedded sensors monitoring structural stress, humidity, and air purity, interconnected with automated HVAC air recovery heat exchangers (HRV) and centralized voice/touch control ecosystems.
Circular Material Recycling
Closed-loop modular components where 95% of structural steel, composite insulation, and exterior alloys can be recovered, repurposed, or fully recycled with minimal cradle-to-cradle carbon penalties.
Turn-Key Sanitary, Multi-Bed & Luxury Expandable Pods
Explore commercial sanitation arrays, luxury glamping pods, multi-bedroom residences, and rapid-response humanitarian shelters.
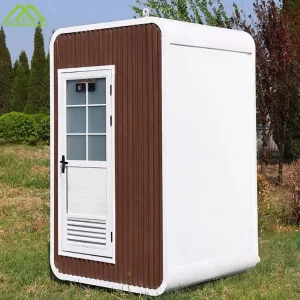
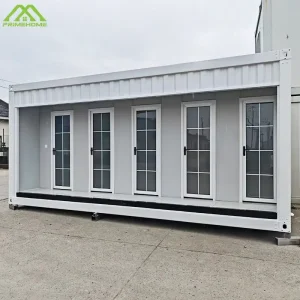
Heavy-duty customized portable container toilets and prefabricated shower containers
Configure Unit Specs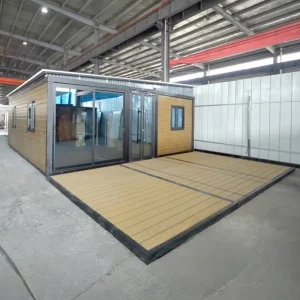
20FT Sloped roof expandable container house with expansive front deck terrace for ADUs
Configure Unit Specs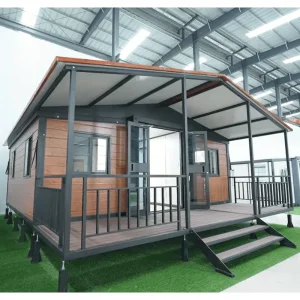
Safe sturdy double wing expandable container house with terrace for youth camps
Configure Unit Specs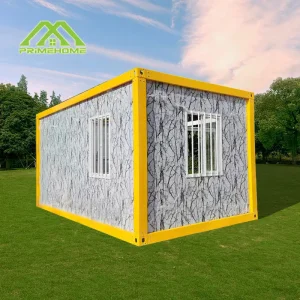
Ready-to-ship modular prefabricated residential housing pods configured with 4 or 5 bedrooms
Configure Unit Specs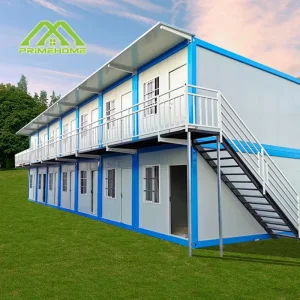
Modular 20ft & 40ft prefabricated container houses with plug-and-play field connections
Configure Unit Specs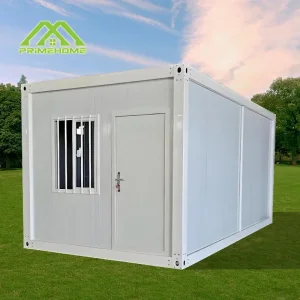
Lightweight modular prefabricated container homes ideal for rapid disaster reconstruction
Configure Unit Specs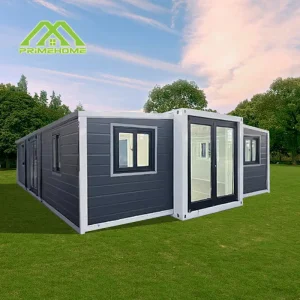
Custom luxury prefabricated double-wing fold-out container home with panoramic glass
Configure Unit SpecsFrequently Asked Questions for Project Developers
Comprehensive engineering, shipping, and structural answers to address complex cross-border procurement challenges.
How do custom container homes prevent condensation and thermal bridging?
We deploy continuous external thermal envelope barriers with non-combustible rockwool or high-density PIR sandwich panels. By avoiding direct thermal contact between internal stud frames and external galvanized skins, and incorporating breathable vapor retarders and mechanical heat-recovery ventilation (HRV), the building prevents interior condensation in all climate extremes.
What foundation requirements apply to expandable and modular units?
Because our structural steel chassis distributes loads along reinforced perimeter corner castings, container homes do not mandate full-slab concrete foundations. Suitable foundations range from concrete strip footings and isolated pier pads to ground screw systems, significantly cutting excavation overhead and environmental impact.
How are units packaged to maximize shipping logistics?
Depending on unit taxonomy, flat-pack and foldable container houses are bundled down to 1/4 of their erected height, enabling up to 4 to 6 units to fit inside a single standard 40ft High Cube container. Pre-finished luxury units like Apple Cabins and Space Capsules ship as completely assembled volumetric pods on flat-rack equipment.
Can internal layouts and luxury appointments be customized per batch?
Yes. Our in-house architectural CAD/BIM team customizes partition placements, smart home automation, high-end stone/composite finishes, custom cabinetry, ADA-compliant accessibility designs, and commercial-grade culinary fittings for bespoke resort and housing developments.
What is the projected architectural design life and warranty structure?
All load-bearing hot-dip galvanized structural steel skeletons carry a 20-year structural warranty, engineered for a service life exceeding 35 to 50 years under standard maintenance. External anti-corrosive multi-coat polyurethane finishes protect against marine salt-spray and UV degradation.
How do you guarantee quality control during bulk procurement runs?
Every production phase undergoes ISO 9001-certified factory inspection checkpoints: raw steel weld ultrasonic testing, multi-point hydro testing on all integrated water lines, electrical insulation megohmmeter verification, and complete monsoon water-spray enclosure simulation prior to export packing.