Turnkey Prefabricated Modules & Panelized Assembly Systems
Explore our top-tier catalog of factory-integrated sanitary units, insulated composite panel walls, and expandable modular structures designed for accelerated deployment and multi-scenario durability.
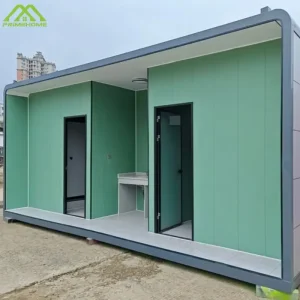
High-Quality Prefabricated Restroom Unit & Portable Bathroom Module
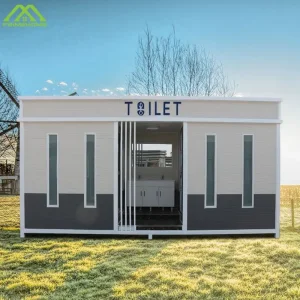
Wholesale Luxurious Prefab Container Toilet with Fast-Install Wall Panels
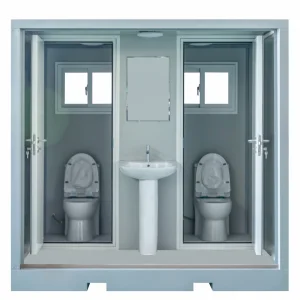
China Modern Integrated Prefab Portable Restroom for Glamping & Resorts
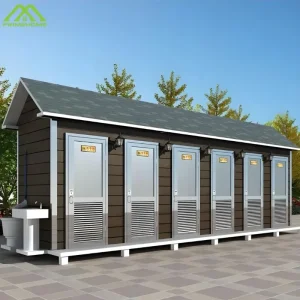
High-Quality Luxury Outdoor Bathroom WC Container Units Wholesale
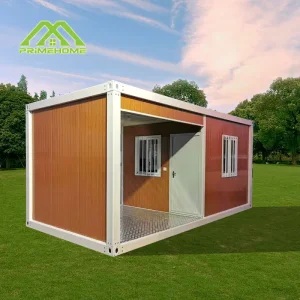
China 20ft/40ft Prefabricated Demountable Structural Container Houses
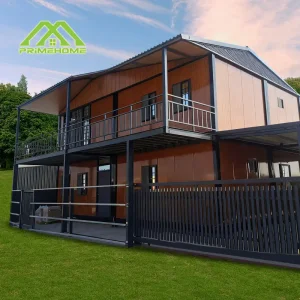
Luxury Residential Modules & Prefabricated Duplex Park Hotel Buildings
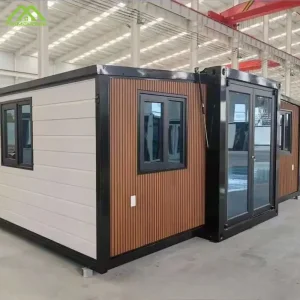
3-Bedroom Luxury Prefab Extension House Foldable Micro Living System
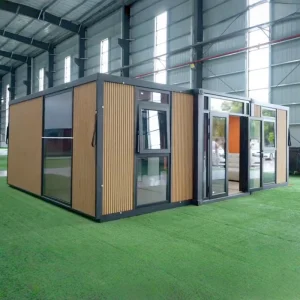
Modern Wooden Grille Design Expandable Modular Home for Eco-Lodging
Navigating Global Panel Procurement: The Industrial Paradigm Shift
Modern EPC contractors, institutional developers, and infrastructure conglomerates face escalating on-site labor shortages, stringent thermal envelope mandates, and compressed development schedules. Custom prefabricated panels represent the cornerstone of off-site manufacturing (OSM).
Envelope Thermal Integrity & R-Value Continuity
Global enterprise procurement demands stringent compliance with continuous insulation (ci) standards such as ASHRAE 90.1, Title 24, and the EU Energy Performance of Buildings Directive (EPBD). Traditional stud framing is riddled with thermal bridges that degrade operational efficiency by up to 35%. Custom prefabricated sandwich panels utilize interlocking cam-lock or tongue-and-groove micro-rib joints engineered to eliminate thermal breaks, ensuring continuous air barriers, moisture management, and operational HVAC load savings across 50-year service cycles.
Defeating Skilled Field Labor Deficits
With global construction labor indices showing historic workforce contraction across North America, Europe, and Australasia, reliance on stick-built site craftsmanship introduces severe cost volatility, delays, and quality discrepancies. By migrating envelope fabrication to robotic, climate-controlled factory environments, general contractors replace hundreds of chaotic field trades with precision-scheduled crane-and-erect crews, achieving weather-tight building envelopes in days rather than quarters.
Life Cycle Assessment & Scope 3 Decarbonization
Multinational real estate investment trusts (REITs) and industrial developers are bound by ESG disclosure frameworks (GRESB, LEED Platinum, BREEAM). Factory-manufactured panels optimize raw material utilization with near-zero waste (under 1.5% compared to 15-20% for conventional cast-in-place or stick-frame methods). High-density mineral wool cores and bio-polyols incorporated into insulated metal panels deliver transparent Environmental Product Declarations (EPDs) with documented reductions in embodied carbon.
Macro Industry Solutions: Engineering Classifications & Applications
From large-scale cold-chain logistics hubs to acoustic-critical modular commercial hospitality, customized prefabricated building panels are engineered around specific thermal, fire, structural, and aesthetic requirements.
Insulated Metal Panels (IMP): Cold Chain & Logistics
Engineered for temperature-controlled warehousing, pharmaceutical cold storage, and mega food-processing plants. IMPs incorporate polyurethane (PIR) or polyisocyanurate cores with closed-cell ratios greater than 95%, cladded in zinc-aluminum galvanized steel with PVDF coatings. They guarantee impermeable vapor barriers, withstand aggressive washdowns, and prevent interior condensation while maintaining cryogenic internal conditions without thermodynamic degradation.
Mineral Wool Core Panels: Passive Fire Protection
Essential for dense urban infill developments, high-occupancy civic buildings, data centers, and multi-tenant industrial corridors. Panels feature structural stone-wool cores with fibers oriented perpendicular to the facing sheet to provide superior shear resistance and non-combustibility. Certified under EN 13501-1 Class A1/A2 and ASTM E119, these assemblies maintain structural containment during fire scenarios for up to 4 hours while inhibiting heat transfer.
Light-Gauge Steel (LGS) Integrated Wall Panels
Tailored for fast-track hospitality pods, resort cabins, student housing complexes, and remote staff camps. LGS panels incorporate structural cold-formed galvanized framing (G90/AZ150) pre-sheathed with fiber-cement or calcium silicate boards and pre-installed electrical conduit runs. These lightweight, seismically resilient panels offer seismic drift absorption and hurricane-grade lateral shear loads without requiring heavy secondary crane gear.
| Panel Typology | Core Composition | Standard Thickness | Thermal Performance | Fire Classification | Typical Industrial Target |
|---|---|---|---|---|---|
| PIR/PUR Ultra-Insulated Panel | High-Density Rigid Polyisocyanurate (42 kg/m³) | 50mm - 200mm | λ = 0.020 - 0.022 W/m·K | Class B-s1, d0 / ASTM E84 Class A | Cold-Storage & High-Efficiency Envelopes |
| Structural Mineral Wool Panel | Hydrophobic Basalt Stone Wool (100-120 kg/m³) | 75mm - 250mm | λ = 0.038 - 0.042 W/m·K | Class A1 / EN 13501-1 (Up to 240 mins) | Data Centers, Substations, Hazardous Warehousing |
| Structural Insulated Panel (SIP) | Expanded Polystyrene (EPS) or Neopor® | 100mm - 300mm | λ = 0.031 - 0.035 W/m·K | B1 Flame Retardant / UL 94 | Modular Residential, Prefab Duplex Villas |
| Architectural Acoustic Panel | Micro-Perforated Steel + Composite Core | 50mm - 120mm | Rw = 32 - 46 dB (STC 44+) | Class A2-s1, d0 | Modular Hospitality, Schools & Medical Clinics |
Technological Roadmap: Automated DFMA & The Factory of the Future
Leading prefabricated building panel manufacturers operate at the nexus of Design for Manufacture and Assembly (DfMA), 6-axis robotic roll-forming, and closed-loop building information modeling (BIM).
BIM Level 3 to Direct-to-Machine CNC Roll-Forming
The days of manual blueprint interpretation are obsolete. State-of-the-art factories ingest IFC and Revit geometry directly into factory CNC production lines. Automated cold roll-forming machines slice, punch, countersink, and swage high-tensile steel frame profiles with sub-millimeter tolerance (±0.5mm). Every service penetration, electrical conduit chase, and plumbing notch is pre-machined at high speed, eliminating in-field drilling and structural compromise.
Next-Generation Phase Change & Aerogel Insulative Layers
Material science breakthroughs are drastically reducing panel thickness while amplifying thermal resistance. Pilot factory integrations incorporate silica-aerogel blanket composites and micro-encapsulated Phase Change Materials (PCMs) within panel cavities. These thermal batteries absorb latent heat during peak diurnal periods and discharge it as ambient temperatures plummet, minimizing chiller cycling in harsh desert and tropical climates.
Structural Health Monitoring (SHM) Smart Sensors
Industrial-scale prefabricated panels are increasingly deployed as responsive smart envelopes. Embedded wireless RFID, interstitial humidity sensors, and piezoelectric fiber-optic strain gauges are embedded between core and facing layers. During transit and service life, these micro-transponders stream telemetry on moisture infiltration, structural shear drift, and envelope deflection, empowering predictive asset management for infrastructure owners.
Global Commercial Landscape: Regional Regulations & Sourcing Dynamics
Understanding localized geopolitical regulatory codes, tariff boundaries, and structural wind-load requirements is essential for transnational developers procuring building panels from primary manufacturing hubs.
North America: IBC, UL Assemblies, & Hurricane High-Velocity Zones (HVHZ)
Procuring prefabricated panels for North American projects demands strict conformity with the International Building Code (IBC) 2021/2024, ICC-ES acceptance criteria (AC04/AC05), and UL 263 fire tests. For maritime and southern regions (Florida, Texas, Gulf of Mexico), wall and roof panels must pass Miami-Dade Notice of Acceptance (NOA) cyclic pressure and large-missile impact testing (ASTM E1886/E1996). Factory quality-control regimens must verify heavy-gauge fasteners, thermal-break isolation clips, and sealants capable of resisting negative wind-uplift pressures exceeding 150 psf.
European Union & United Kingdom: CE Marking, Eurocodes, & Fire Safety Regimes
Following regulatory reforms (including the UK Building Safety Act), European buyers mandate EN 14509 Harmonized Standards for factory-made self-supporting double skin metal face insulating panels. Combustibility is subject to scrutiny: PIR formulations must achieve certified Euroclass B-s1, d0 minimum ratings, while residential mid-rise and high-rise facades require non-combustible Class A1/A2 mineral fiber cores. Sourcing factories must furnish verified Factory Production Control (FPC) audit trails and Third-Party Notified Body certifications.
Middle East & GCC: Extreme Heat, Sand Abrasion & Civil Defense Approval
The rapid scale of mega-projects in Saudi Arabia (Vision 2030, NEOM, Red Sea) and the UAE demands panelized solutions that thrive under continuous ambient temperatures of 50°C and UV radiation. Panels require thick polyurethane/PIR cores or dense rockwool, protected by PVDF fluoropolymer or Plastisol coatings resistant to saline humidity and abrasive dust storms. Procurement requires Civil Defense registration, NFPA 285 multi-story exterior wall fire performance verification, and rapid-erection lock fittings for accelerated desert installations.
Australia & New Zealand: NCC 2022, AS/NZS Standards & Bushfire (BAL)
The Australasian construction sector is governed by the National Construction Code (NCC) with mandatory verification under AS/NZS 4859.1 (thermal materials) and AS 1530.1 / AS 1530.4 (fire combustibility and structural resistance). In fire-prone regions, panels must achieve Bushfire Attack Level ratings up to BAL-FZ (Flame Zone). Furthermore, cyclonic zones across Western Australia and Queensland necessitate verified static water penetration tests under AS/NZS 4284, requiring factory tolerance controls that prevent salt-air-induced corrosion.
Supply Chain Engineering: Protective Packing, Logistics & Site Erection
A factory-perfect panel provides zero value if damaged in international transit or misaligned during field crane lifting. High-caliber manufacturers engineer both the product and its deployment logistics.
Engineered Export Bundling & Anti-Corrosion Crating
Intermodal maritime logistics expose panels to condensation, salt spray, and vibration shear. Top manufacturers implement automated protective film application, closed-cell corner guards, and vacuum-sealed desiccant packaging within specialized steel pallet cassettes. Panels are stacked in inverted male-female orientations to optimize ocean freight volume in high-cube shipping containers, keeping total cubic meter logistics expenses minimized.
Sequenced "Just-In-Time" Delivery Schedules
Urban construction sites have negligible laydown footprints. Utilizing integrated RFID tracking and QR-coded panel labeling, crates are unloaded directly from flatbeds to cranes according to real-time structural sequence. Every bundle corresponds to precise floor and grid references within the master BIM model, eliminating chaotic sorting and double-handling while safeguarding panel surfaces from on-site mechanical scarring.
Field Connection Detailing & Lifting Protocols
Field productivity depends upon integrated lifting eyes and factory-approved non-destructive vacuum lifters. Panel connections feature concealed fixings with hidden fasteners protected by continuous overlapping metal joints. Self-drilling bimetallic screws, butyl mastic seals, and expanding EPDM weather-strips guarantee airtight perimeter seals, enabling installation crews to secure up to 800 square meters of facade per single crane shift.
Factory Verification: The Technical Due-Diligence Checklist
Before awarding high-volume panel contracts, global enterprise procurement teams must conduct rigorous factory audits. Verify that your supply chain partner operates according to standardized international manufacturing controls.
1. Raw Material Metallurgy & Chemical Purity
Verify mill test certificates (MTC) for coil steel: minimum yield strength of 280-350 MPa, minimum metallic zinc coating of 275 g/m² (Z275) or AZ150. For polyurethane cores, check high-pressure metering foaming machines (KraussMaffei or Hennecke) ensuring uniform closed-cell densities and ZERO ozone depletion potential (ODP) hydrofluoroolefin (HFO) blowing agents.
2. Continuous vs. Discontinuous Production
High-output commercial orders require high-speed continuous double-belt lamination lines with heated conveyor beds up to 35 meters in length. Continuous lamination guarantees complete chemical adhesion between sheet metal facings and core foam, avoiding core voids, delamination under heat exposure, and thermal blistering over long service horizons.
3. In-House Quality Testing Laboratories
Legitimate manufacturers run continuous destructive and non-destructive laboratory tests: flatwise tensile strength testing (EN 1607 / ASTM C297), cross-breaking shear load verification, thermal conductivity guarded hot box assessments (ISO 8301), and accelerated cyclic salt-spray corrosion chambers (ASTM B117) to provide verifiable compliance data per production batch.
Factory-Built Modular Units & Expandable Habitat Envelopes
Review our extensive range of high-efficiency modular container units, expandable multi-bedroom houses, and specialized sanitary modules ready for intermodal export and instant commissioning.
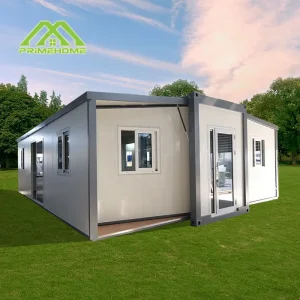
Outdoor Modern Mobile Home with Bathroom Sustainable & Collapsible
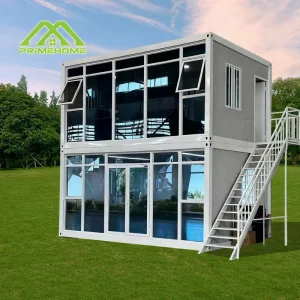
Modular Demountable Hotel with Solar & Energy Storage Integration
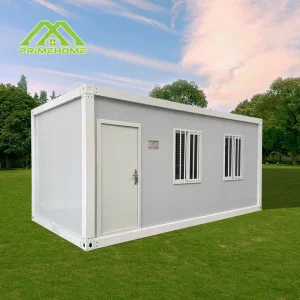
Custom 20ft Prefabricated Foldable Container House for Camp Apartments
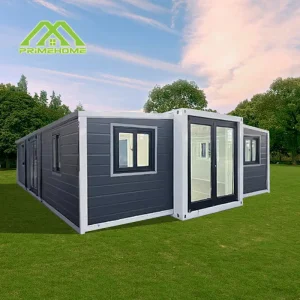
Luxury Double-Wing Expandable Container House Readymade Fold-Out Villa
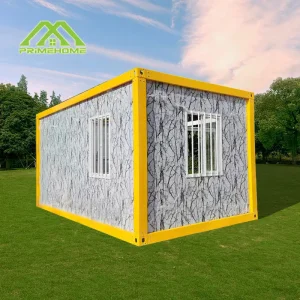
Prefabricated Modular Multi-Bedroom Container Houses (4-5 Bedrooms)
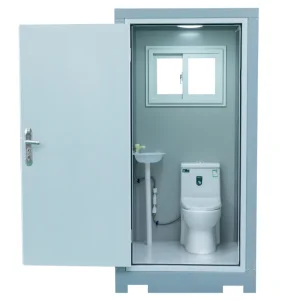
Outdoor Portable Public Restroom Prefab Porta Potty for Parks & Camping
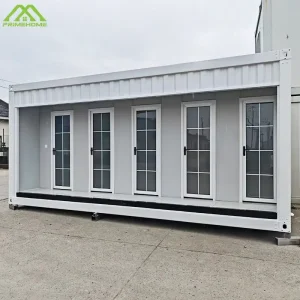
Custom Portable Container Toilets & Prefab Shower Container Facilities
Modularized Detachable Houses with Complete Kitchen & Sanitary Enclosures
Frequently Asked Technical & Procurement Inquiries (FAQ)
Detailed technical answers to common engineering questions concerning custom prefabricated panels, structural compliance, logistics, and longevity.
How do custom prefabricated building panels prevent long-term interstitial moisture and vapor condensation?
Prefabricated composite panels address moisture through impermeable continuous metal outer facings and precision-engineered vapor-tight joints. Premium sandwich panels feature dual tongue-and-groove micro-gaskets factory-injected with non-setting butyl sealants. This establishes a continuous air and vapor barrier on the warm side of the insulation, eliminating convective air pathways. When third-party tested according to ASTM E283 (air leakage) and ASTM E331 (water penetration), these interlocking systems achieve zero water entry at test pressures exceeding 15 psf (720 Pa), preventing internal cavity mould, rust, and insulation R-value degradation.
What fire-resistance test standards are required for multi-story panelized applications?
For commercial multi-story facades and industrial partitions, the primary benchmarks include ASTM E119 / UL 263 (fire tests of building construction and materials) in North America and EN 1365-1 / EN 13501-2 in Europe. For exterior facade propagation, panels must satisfy NFPA 285 (standard fire test method for evaluation of fire propagation characteristics of exterior non-load-bearing wall assemblies) or British Standard BS 8414. Structural stone mineral-wool panels with densities between 100-120 kg/m³ achieve up to a 4-hour non-combustible fire rating (EI240), preserving structural load capacity while emitting zero toxic gas or burning droplets.
Can prefabricated panels be customized to match bespoke architectural finishes and curved profiles?
Yes. Modern computerized continuous laminating lines and off-line press-brake machines permit customized external steel skins, including architectural micro-rib, shadow-line, striated, embossed stucco, and completely flush cassette visuals. Coating systems range from standard 25-micron polyester coatings to high-durability 50-micron PVDF (polyvinylidene fluoride) and polyurethanic finishes that resist chalking and UV bleaching. Panels can also receive factory-laminated exterior architectural accents such as real-wood grilles, stone-polymer composite facades, or terracotta rainscreen systems via integrated hidden rail clips.
What is the structural life expectancy and warranty coverage of factory-direct panels in harsh maritime environments?
In coastal environments classified under ISO 12944 Corrosivity Categories C4 (high marine) and C5 (very high marine), panel durability depends heavily on substrate metallurgy and coating technology. Specifying Hot-Dip Galvalume® steel (55% Al-Zn alloy, AZ150/AZ185) or ZAM (Zinc-Aluminum-Magnesium alloy) paired with heavy-duty fluoropolymer finishes provides an operational design service life exceeding 35 to 50 years. Standard factory warranties provide 15 to 25 years against film integrity failure, structural core delamination, and perforative corrosion when installed with matched austenitic stainless-steel (Grade 304/316) fasteners.
How are MEP (mechanical, electrical, plumbing) services integrated into custom building panels?
During automated factory prefabrication, electrical conduits, outlet back-boxes, and plumbing line chases are routed into the insulation core prior to lamination, governed by the engineer’s coordinated BIM MEP collision model. For structural light-gauge steel (LGS) panels, service holes are pre-punched with flanged grommet collars directly into the steel studs by automated CNC mills. This enables rapid field wire pull-through and pipe joining without requiring abrasive wall trenching or compromising the continuous insulative envelope.
What documentation and certifications should accompany international containerized panel shipments?
Every international export shipment must be accompanied by a comprehensive technical compliance dossier. This includes: Raw Material Mill Test Certificates (MTC) proving steel tensile yield strength and coating weights; Core Density and Thermal Conductivity Test Reports (ISO 8301 / ASTM C518); Third-Party Fire Reaction & Resistance Certifications (UL, CE EN 14509, AS 1530); Container Loading & Moisture Desiccant Reports; and a Project-Specific Erection Drawing Set indicating sequential panel identification numbers matching the external pallet shipping manifests.